August 10, 2026
Why Blue Gloves Dominate Food Processing
August 10, 2026
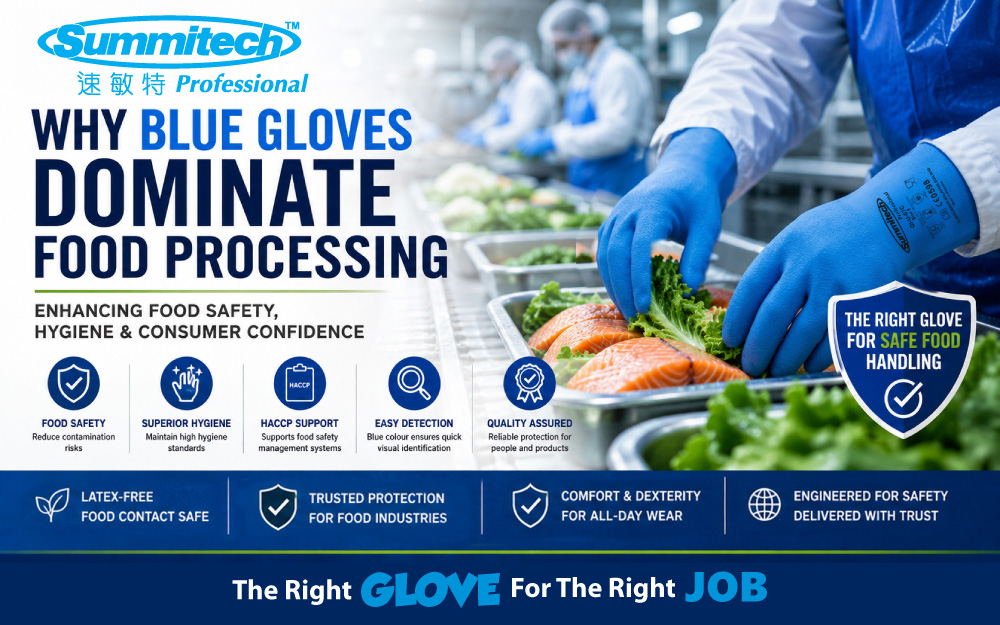
Walk into almost any food manufacturing plant, commercial kitchen or food processing facility, and you'll notice one common detail - workers are almost always wearing blue gloves.
This isn't a branding preference or fashion choice. The widespread use of blue gloves is the result of decades of food safety practices, risk management and international industry standards.
Colour plays an important role in preventing contamination, improving product inspection, and protecting consumer health. While gloves are primarily designed to protect workers and food products, selecting the correct glove colour can significantly enhance food safety systems.
At Sumirubber Malaysia, our Summitech Professional food handling gloves are designed to support hygiene, compliance and operational efficiency. Understanding why blue gloves have become the industry standard helps businesses make informed decisions when selecting hand protection.
Every food manufacturer follows one common objective:
Prevent contamination before it reaches the consumer.
While much attention is given to glove material, food-grade certification and hygiene practices, glove colour is another important element of contamination control.
An easily visible glove allows workers to quickly identify tears, damage or contamination before food products are affected.
Blue is rarely found naturally in food.
Unlike white, beige or transparent gloves, a blue glove fragment is much easier to detect if it accidentally enters the production process.
This simple advantage allows workers to quickly identify contamination during:
The result is faster corrective action and reduced product loss.
Many food manufacturers operate under Hazard Analysis and Critical Control Point (HACCP) systems.
One objective of HACCP is to minimize every possible contamination risk.
Blue gloves support HACCP by making foreign material easier to detect during production.
Although HACCP does not specifically require blue gloves, many companies adopt them as a best practice because they improve visibility and reduce contamination risk.
Modern food processing facilities operate at high speed.
Workers inspect hundreds or even thousands of products every hour.
A bright blue glove provides strong visual contrast against foods such as:
This visibility makes it easier to identify:
Quality inspectors rely heavily on visual detection.
Blue gloves help quality teams quickly identify:
This contributes to more effective quality assurance throughout the production process.
Some specialised food handling gloves are manufactured with metal-detectable properties.
These gloves contain detectable additives that can be identified by metal detectors or X-ray inspection systems.
When combined with their distinctive blue colour, they provide two layers of contamination protection:
This combination further strengthens food safety programmes in high-risk production environments.
Although blue gloves are preferred, colour alone does not guarantee food safety.
Food handling gloves should also provide:
Selecting the appropriate glove material remains equally important.
Different food applications require different glove materials.
Nitrile Gloves
Suitable for:
Benefits include:
Natural Rubber Gloves
Suitable for:
Benefits include:
PVC Gloves
Suitable for:
Benefits include:
Choosing the correct glove depends on the specific task, food type and operational risks.
Food processing employees often wear gloves for several hours every day.
Comfortable gloves encourage workers to:
Poorly fitting gloves can decrease productivity and increase the likelihood of workers removing their PPE.
To maximise food safety:
Remember, gloves are only effective when they are used correctly.
At Sumirubber Malaysia, our Summitech Professional food handling gloves are developed to meet the demanding requirements of modern food processing industries.
Our solutions are designed to provide:
Whether used in food manufacturing, commercial kitchens, seafood processing or packaging operations, our gloves help businesses maintain high standards of hygiene and worker protection.
Blue gloves have become the preferred choice in food processing because they improve visibility, support contamination control and strengthen quality assurance systems.
However, colour is only one part of an effective glove selection strategy. The right combination of glove material, comfort, durability and food-contact compliance is essential for protecting both workers and consumers.
By understanding why blue gloves dominate the industry, businesses can make better PPE decisions that improve food safety, operational efficiency and customer confidence.
At Sumirubber Malaysia, we remain committed to delivering trusted Summitech Professional hand protection solutions that help food manufacturers achieve the highest standards of safety and quality.
Understanding Sustainability, Performance & the Future of Hand Protection
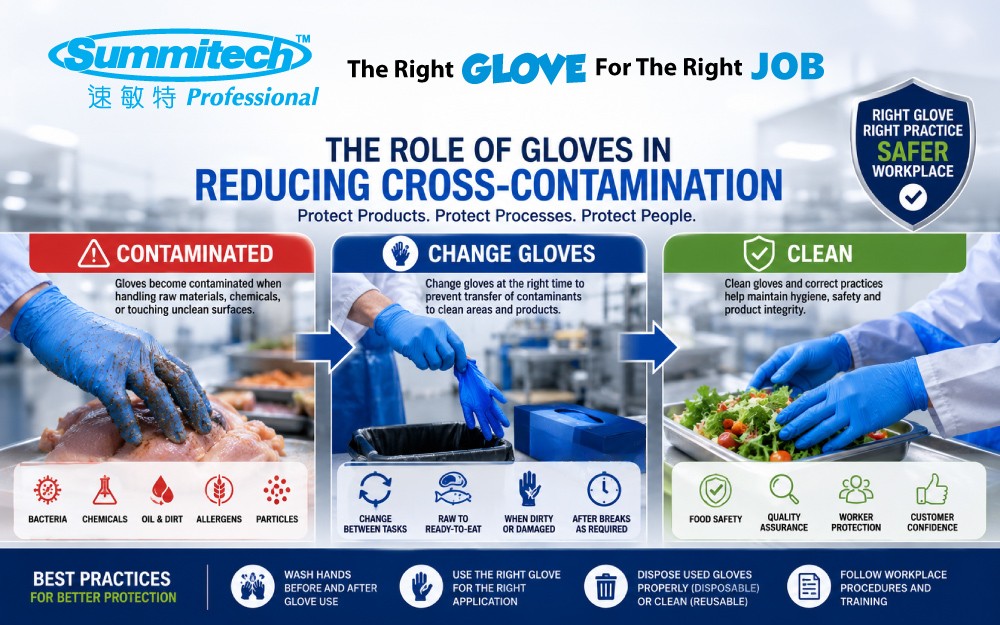
How Propoer Glove Use Protects Products, Processes & People
Glove Thickness Explained: Finding the Right Balance Between Protection and Dexterity When selecting industrial gloves, one of the first specifications buyers often compare is…